Pasteurization

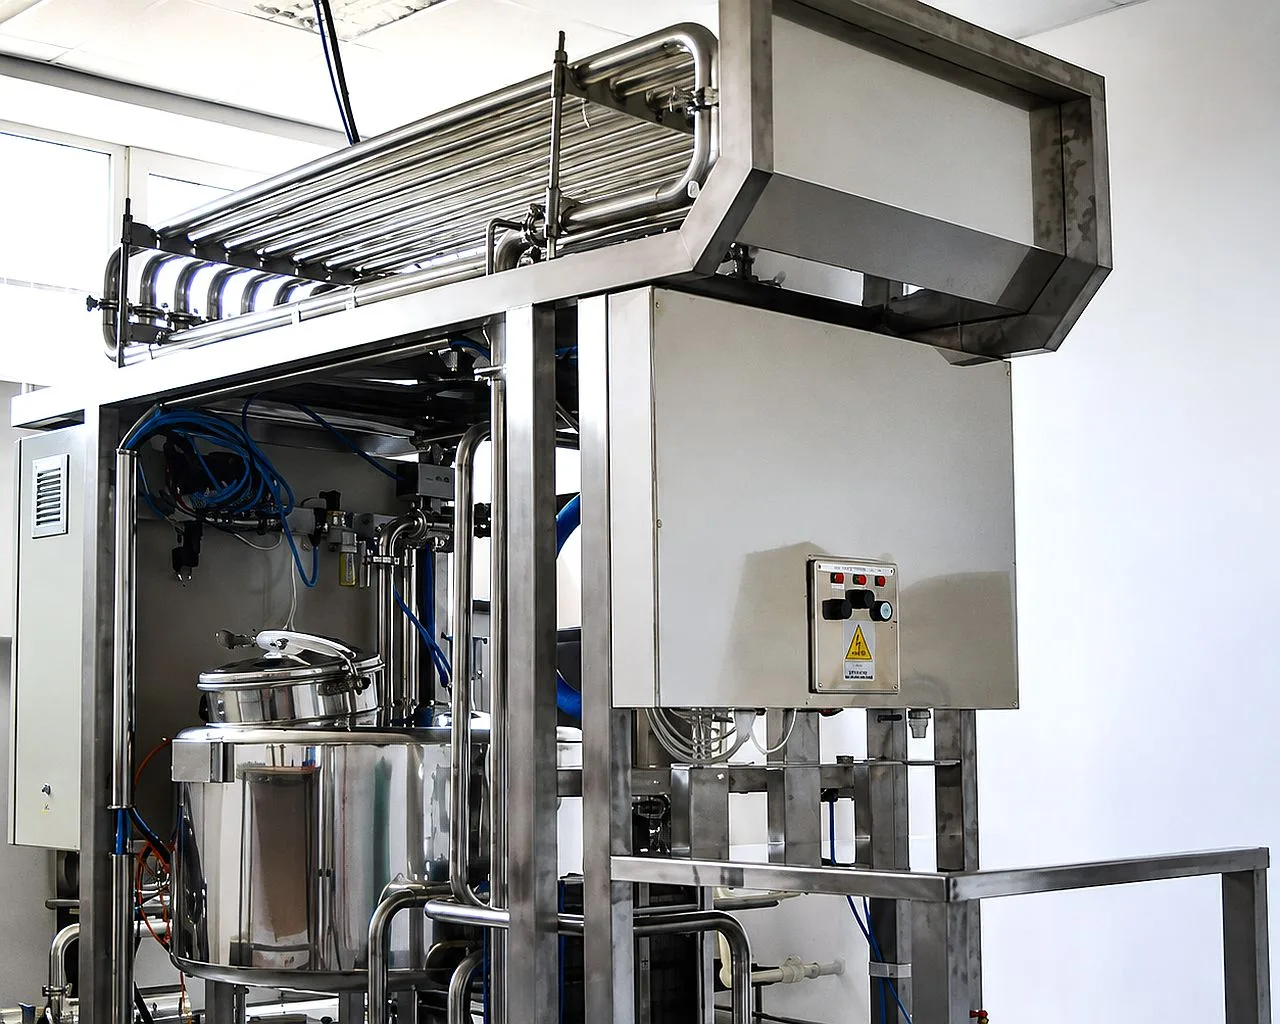
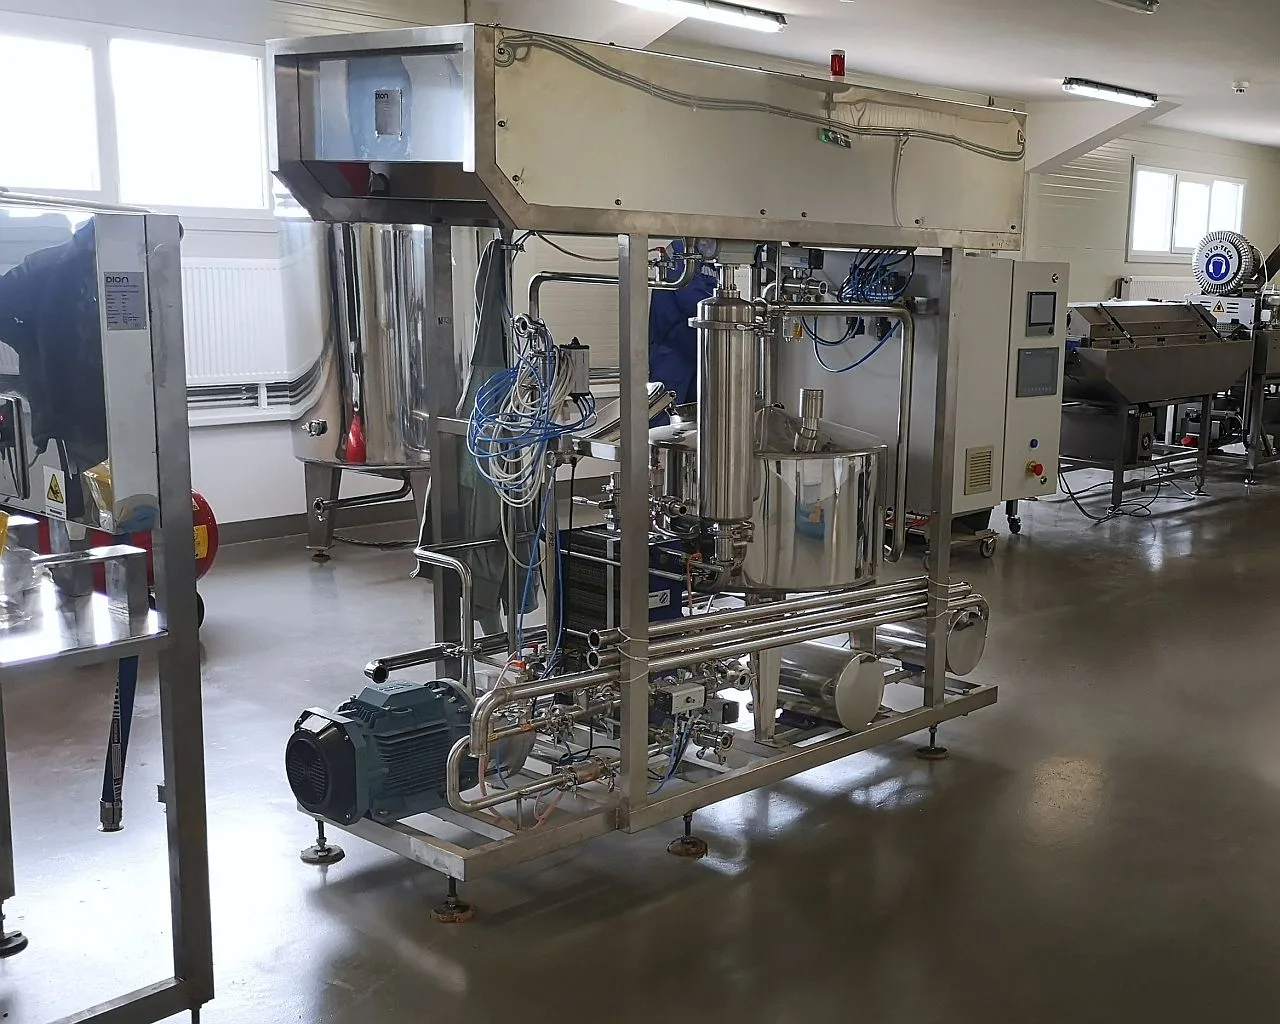
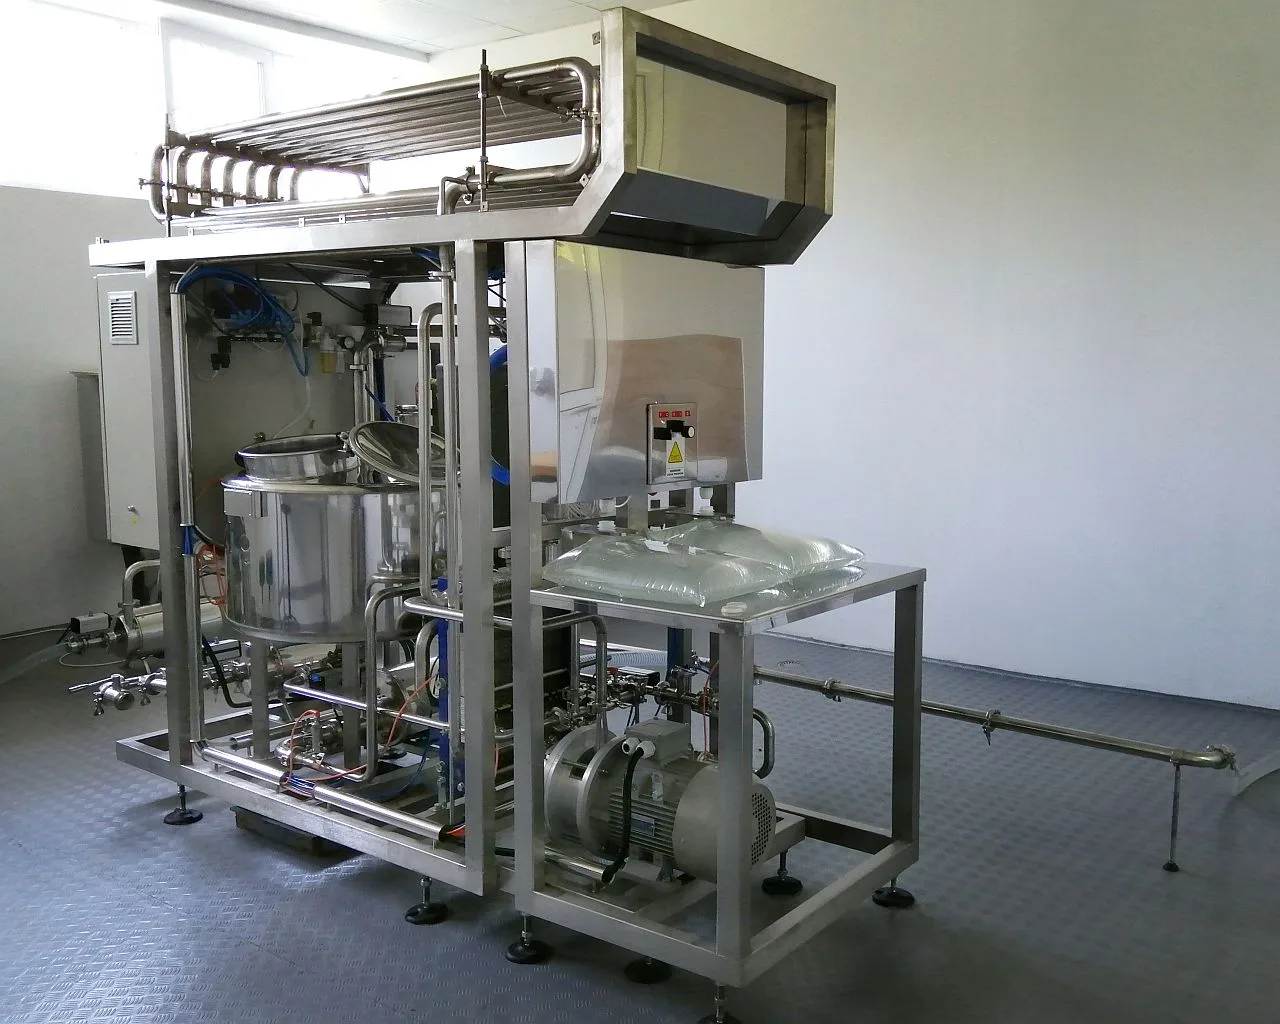
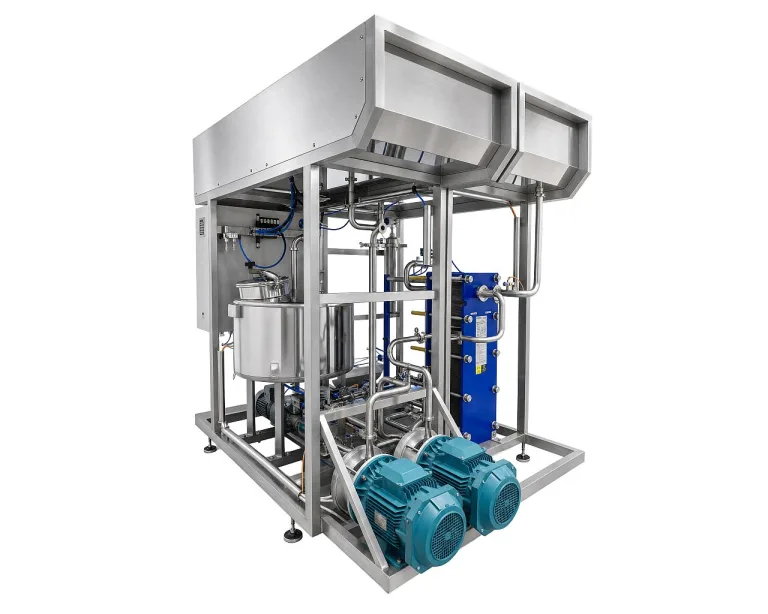
OPS-1000/1500 liquid egg pasteurizer

Available within 3 months
  • 1000-1500 L/h (approx. 19,000 – 28,500 eggs/hour)
  • Integrated Pasteurization & Filling
    The system automates the entire process of heat treatment, rapid cooling, and precision dosing of liquid eggs directly into Bag-in-Box packaging.
  • No steam or gas boiler required
    RSH rotor ensures exceptionally gentle homogenization, preserving 100% of protein functional properties (foaming, emulsifying, coloring) at fresh-egg quality levels.
  • 8-hour continuous operation
    Direct heating eliminates burning and fouling, allowing non-stop operation without intermediate cleaning.

Product description

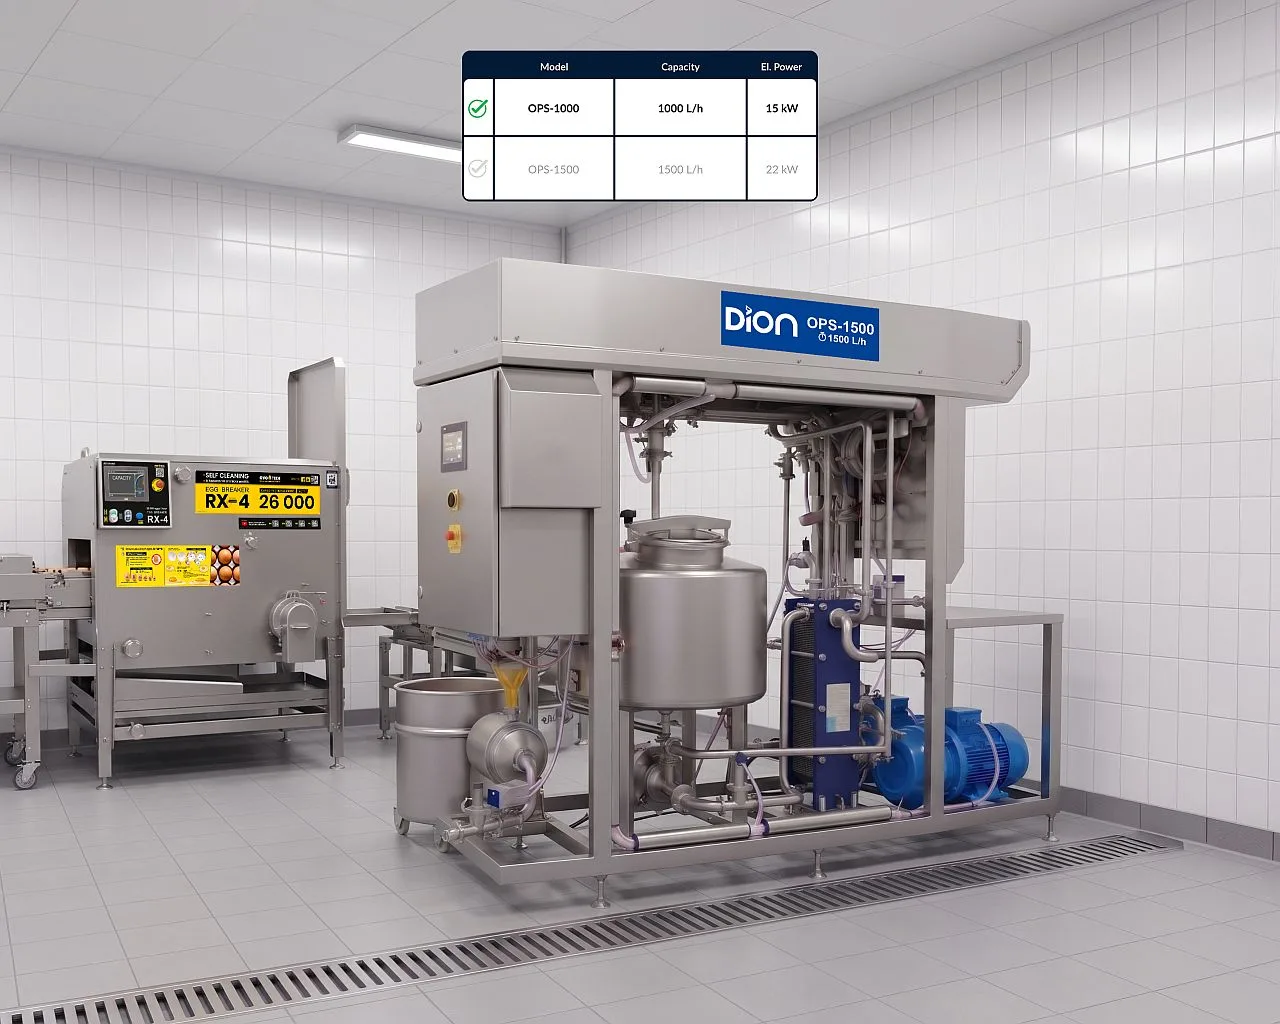
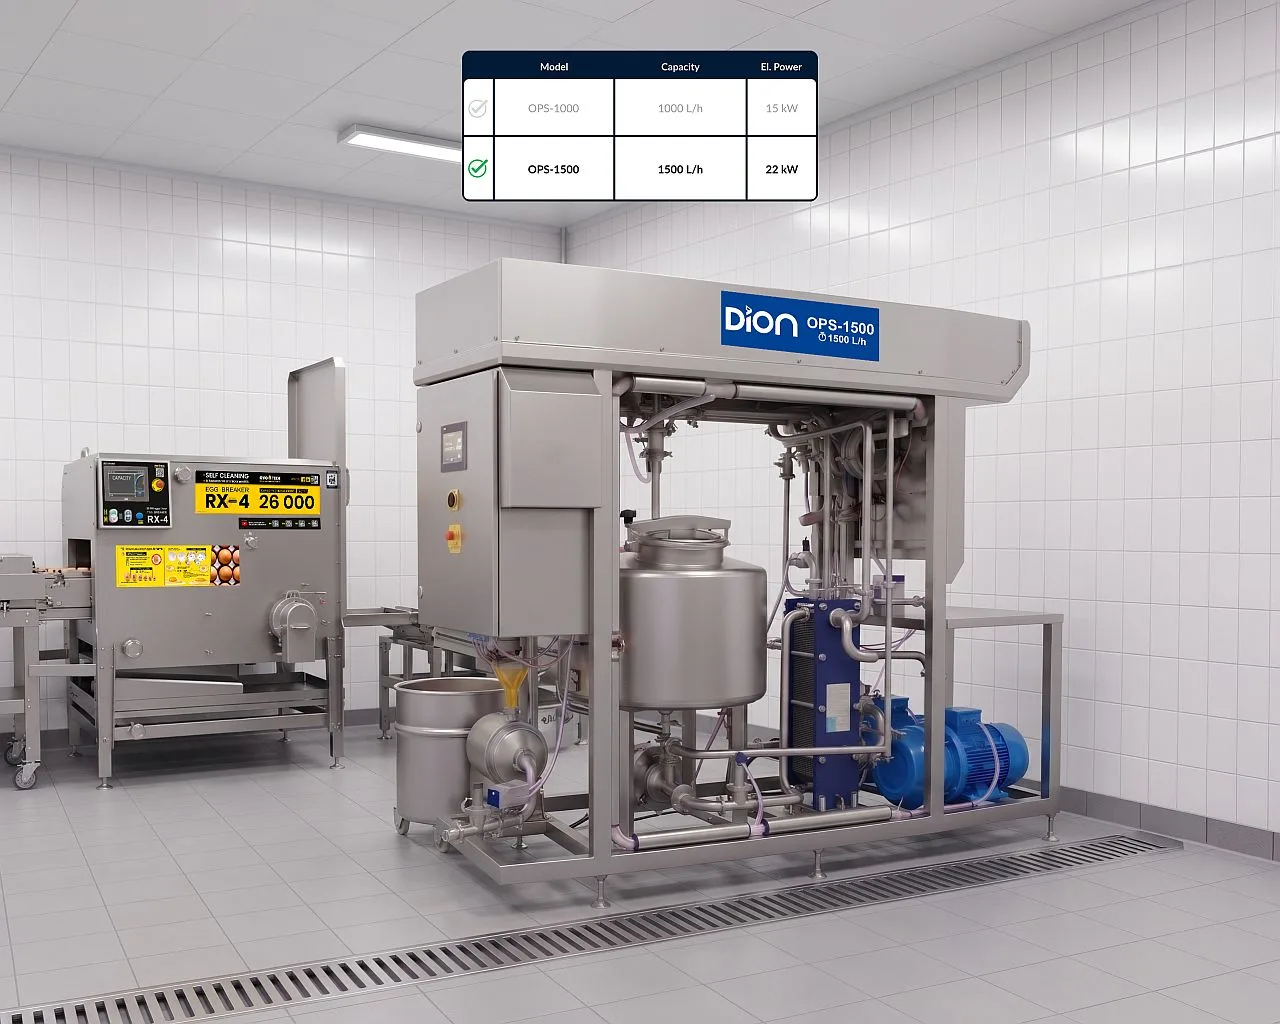
Designed for medium-scale egg processing facilities, the OPS-1000/1500 liquid egg pasteurizer incorporates patented RSH (Rotor Spinning Heater) technology. This solution provides energy-efficient thermal treatment and gentle homogenization without external boilers or high-pressure homogenizers. Direct heating prevents fouling, ensuring continuous operation and maximum protein quality retention.

OPS 1000 RSH: Capacity of 1,000 l/h (approx. 19,000 eggs/hour) | Power: 15.0 kW
OPS 1500 RSH: Capacity of 1,500 l/h (approx. 28,500 eggs/hour) | Power: 22.0 kW

Automates preheating, pasteurization, 180-second holding, and rapid cooling. Compatible with aseptic Bag-in-Box filling and bulk containers.

Compatibility:

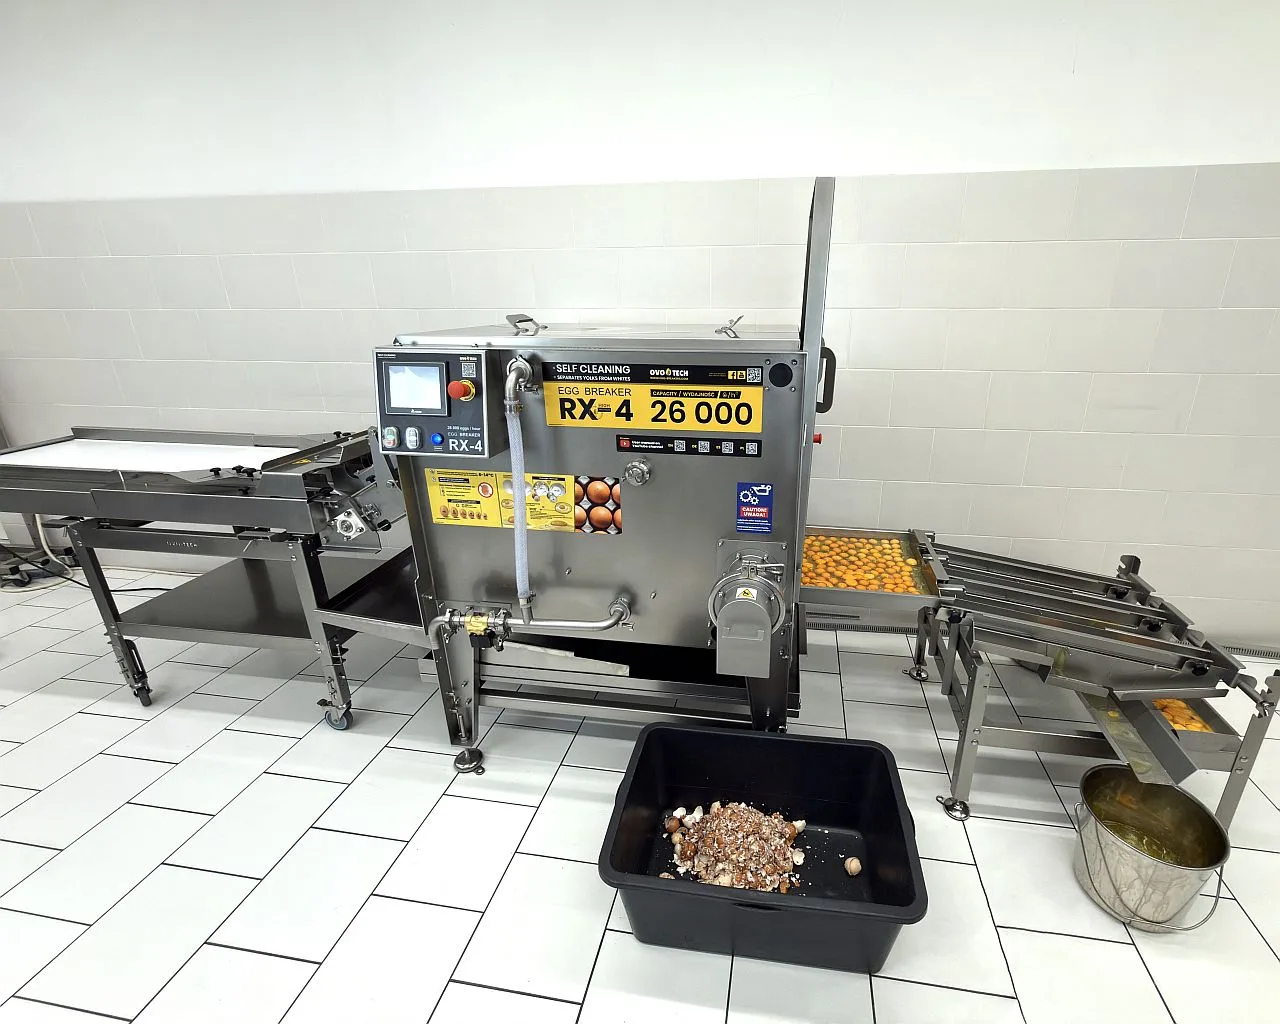
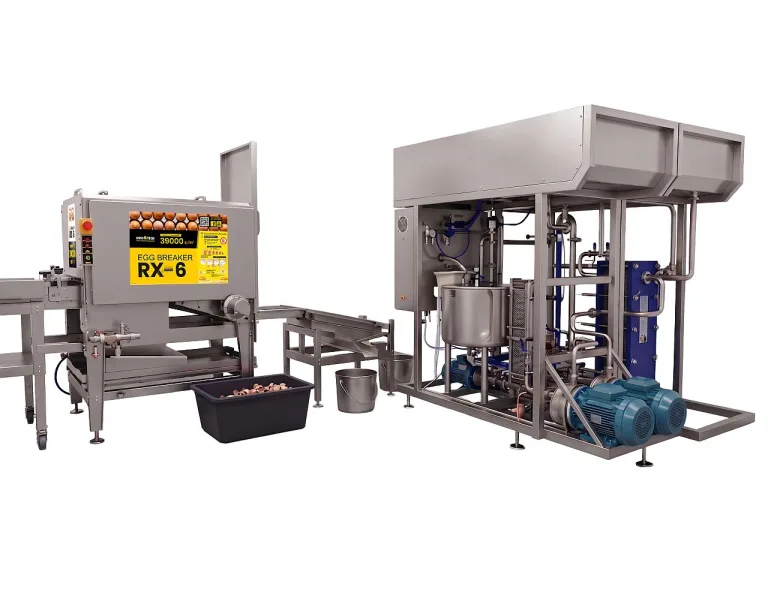
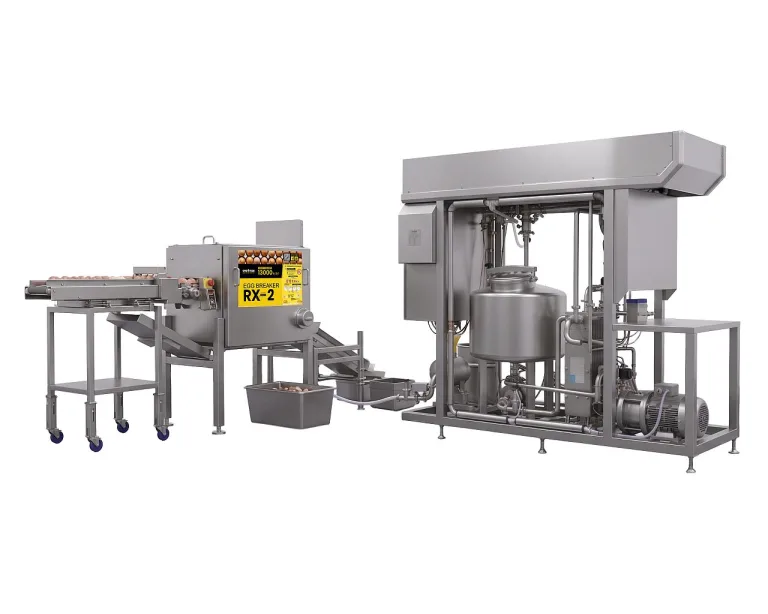
RX-4, MX-4, FM Filling Machine, OVO-TANK liquid egg storage system

FAQ

What is the pasteurization temperature?
The pasteurization temperature is tailored to the specific raw material: Liquid whole egg (melange) 62°C – 67°C, Liquid egg white 50°C – 55°C, Liquid egg yolk 62°C – 70°C
How long does the pasteurization process take?
To ensure effective pasteurization, the product is held for a holding time of 180 seconds.
Do I need a separate homogenizer with a pasteurizer with RSH technology?
No. The pasteurizer equipped with an RSH heater performs gentle in-line homogenization directly during the pasteurization process. A conventional homogenizer involves high capital expenditure (CAPEX) and energy consumption—with RSH technology, you save both energy and investment costs.
How is the product packaged and filled after pasteurization?
After cooling, the product can be fed directly into automatic or semi-automatic filling machines for packaging into Bag-in-Box containers, bottles, or IBC bulk containers (totes / pallecons).
What are the key advantages of RSH Technology?
Stable and precise process temperature control with an accuracy of ±0.1°C. The RSH rotor delivers exceptionally gentle homogenization while extending continuous operation to 8–10 hours without the need for intermediate cleaning.

Technical parameters

Capacity1000-1500 L/h (approx. 19,000 – 28,500 eggs/hour)
MaterialINOX EN 1.4301 (AISI 304)
Power15.0-22.0 kW
Pasteurization holding time180s
Process automationPLC/HMI
Integrated CIP (Clean-In-Place) systemIncluded
Optional integrationBag-in-Box and bulk container filling systems

    Contact Form

    Similar products

    Pasteurization

    OPS-3000/10000 liquid egg pasteurizer

    Available within 3 months
    • 3000-10000 l/h (approx. 57,000 – 190,000 eggs/hour)
    Recommended for industries
    Confectionery & Bakery Catering HoReCa Pasta production
    Pasteurization

    OPS-2000 liquid egg pasteurizer

    Available within 3 months
    • 2000 L/h (approx. 38,000 eggs/hour)
    Recommended for industries
    Confectionery & Bakery Catering HoReCa Pasta production
    Pasteurization

    OPS-200/500 liquid egg pasteurizer

    Available within 3 months
    • 200-500 L/h (approx. 3,800 – 9,500 eggs/hour)
    Recommended for industries
    Confectionery & Bakery Catering HoReCa Pasta production